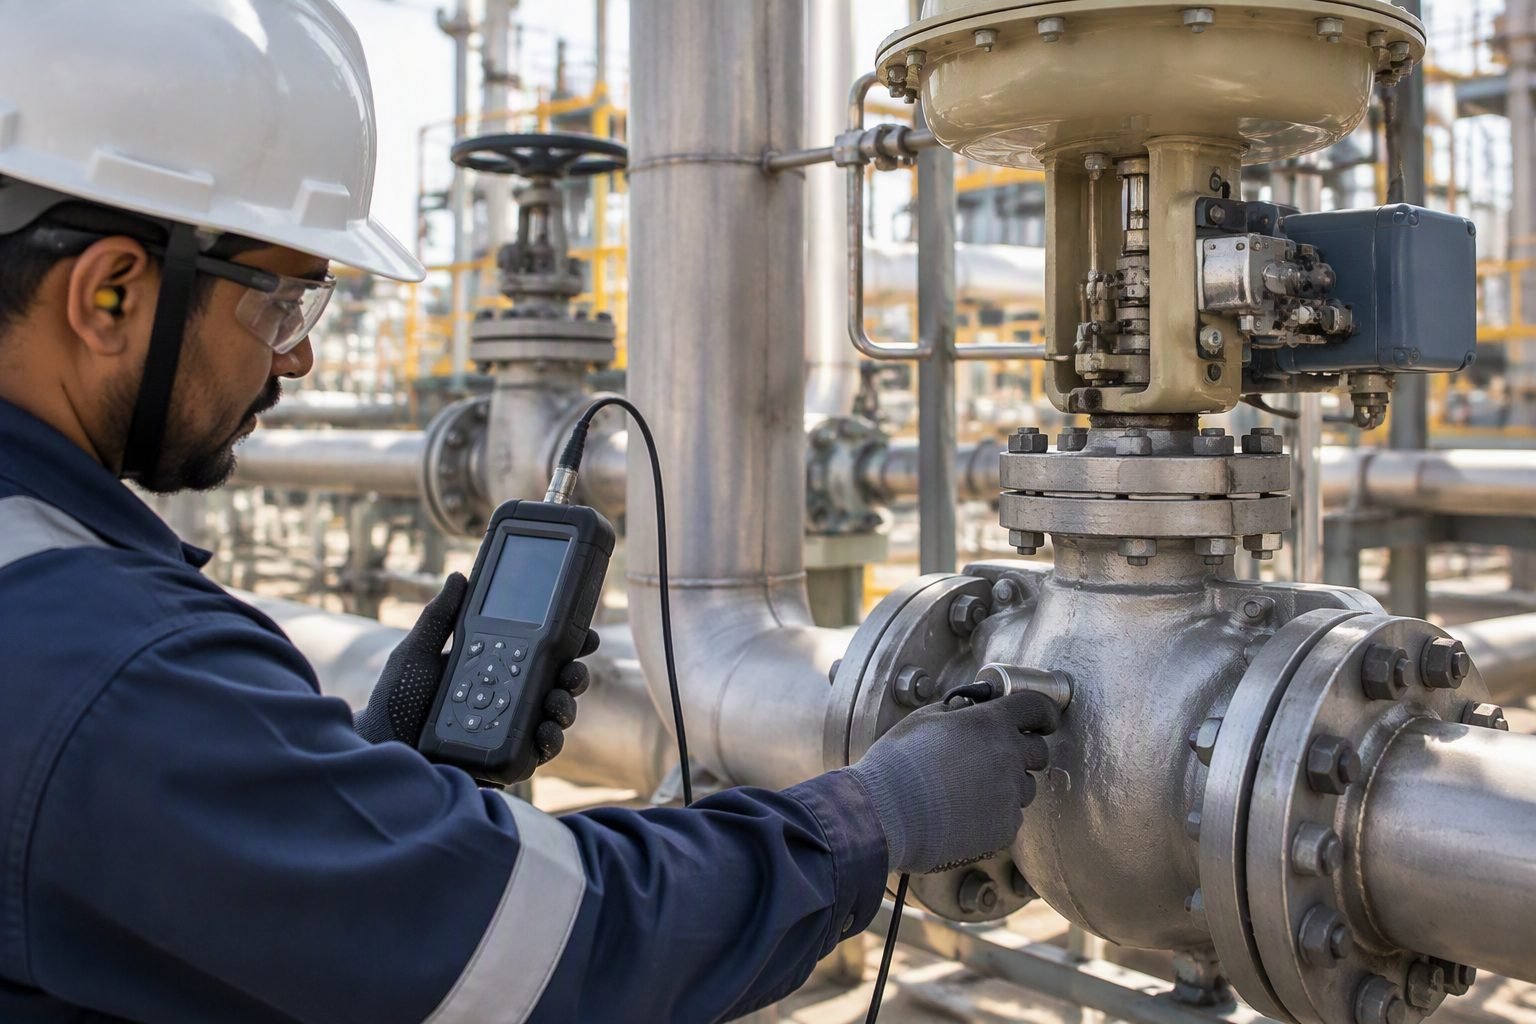
Mastering NACE MR0175 Material Verification for Sour Valve Trim
In my twenty years of designing piping systems for sour service oil and gas production facilities, I have learned that overlooking a single material test certificate can result in catastrophic sulfide stress cracking within months of commissioning. When specifying critical valve trim components such as stems, plugs, and seat rings, relying solely on standard mill test reports is never sufficient. Sour service environments containing wet hydrogen sulfide demand rigorous metallurgical controls, strict hardness thresholds, and complete traceability back to the original melt.
This guide outlines the complete engineering framework required to verify material compliance for valve trim operating under corrosive hydrocarbon conditions. We will examine the metallurgy of sulfide stress cracking, establish protocols for hardness verification, and align your procurement documentation with international petroleum standards to eliminate field failures.
Key Engineering Takeaways
- Enforce a strict maximum hardness ceiling of 22 HRC for carbon and low alloy valve trim steels.
- Validate all Material Test Reports against chemical composition limits defined in NACE MR0175 / ISO 15156 Part 3.
- Perform independent positive material identification and hardness testing on 100% of critical trim components prior to shop assembly.
NACE Compliance Engineering Framework for Sour Service Valve Trim
When hydrogen sulfide dissolves in free water within process piping, it generates hydrosulfide ions that inhibit the recombination of hydrogen atoms on steel surfaces. These atomic hydrogen atoms diffuse into the crystal lattice of high-hardness valve trim components, accumulating at microstructural traps and grain boundaries. Under sustained tensile stresses, this localized hydrogen concentration causes brittle failure mechanisms known as sulfide stress cracking and hydrogen-induced blistering.
To mitigate these failure modes, ISO 15156 / NACE MR0175 establishes strict manufacturing parameters. Valve stems, which experience high cyclic bending and torsional loads, require specialized austenitic stainless steels or nickel-based alloys that maintain resistance without exceeding critical yield strength boundaries.
Hardness Limitations and Heat Treatment Controls
Hardness serves as the primary field-measurable proxy for tensile strength and susceptibility to hydrogen embrittlement. For common carbon steels, low alloy steels, and martensitic stainless steels used in valve trim applications, the maximum allowable hardness is capped at 22 HRC. Exceeding this threshold exponentially increases susceptibility to sulfide stress cracking, even at low operating stress levels.
Achieving this hardness limit requires precise control over quenching and tempering cycles during component manufacturing. Austenitizing temperatures, cooling rates, and tempering soak times must be documented on the production heat treatment charts. Any deviation from approved furnace parameters mandates complete re-heat treatment and re-testing.
Critical Engineering Warning: Hardness Testing Locations
Surface decarburization or localized cold work from machining can produce artificially low or high hardness readings on valve trim surfaces. ASME and NACE standards require hardness indentations to be placed on cross-sections representative of the heaviest section thickness, specifically in areas subjected to maximum operational stress such as stem roots and plug seating diameters.
Using portable Leeb rebound testers on finished machined surfaces is unacceptable for final compliance sign-off; Rockwell bench testing on sacrificial coupons or finished components is mandatory.
Material Test Report Verification Protocols
A Material Test Report functions as the primary legal and technical guarantee of metallurgical integrity. During engineering review, piping designers must audit every line item of the MTR against the raw material specification and NACE compositional limits. Particular attention must be paid to residual elements such as sulfur, phosphorus, and carbon equivalents, which directly influence cracking susceptibility.
- Verify that the heat number stamped on the physical valve trim component matches the heat number recorded on the certified mill test report.
- Confirm that chemical analysis encompasses all specified alloying elements, including nickel, chromium, molybdenum, and controlled micro-alloy additions.
- Check mechanical test results for actual tensile strength, yield strength, and elongation against ASME B16.34 minimum requirements.
- Ensure the testing laboratory operates under accredited quality systems such as ISO 17025 certification.
Alloy Selection Matrix for Severe Sour Service
As partial pressures of hydrogen sulfide increase in high-pressure gas production, standard martensitic trims like ASTM A276 Type 410 become unsuitable due to chloride stress corrosion cracking and hardness restrictions. Engineers must transition to solid corrosion-resistant alloys that derive their strength from solid solution hardening rather than martensitic transformation.
Alloys such as UNS N06625, UNS N10276, and specialized duplex stainless steels offer exceptional resistance in severe sour environments. However, these materials introduce distinct welding and fabrication challenges that require strict adherence to pre-qualification standards and specialized filler metal selection.
Advantages
- Eliminates catastrophic sulfide stress cracking and sudden pressure boundary failures in sour gas lines.
- Ensures full regulatory compliance with international oil and gas safety standards like ISO 15156.
- Extends valve operational lifespan and reduces unexpected plant shutdown frequency.
- Provides verifiable quality traceability from raw ingot melt to final installed valve trim.
- Lowers overall plant insurance risk profiles by mitigating catastrophic environmental release hazards.
Disadvantages
- Increases initial procurement lead times due to specialized metallurgical testing requirements.
- Requires higher capital expenditure for corrosion-resistant alloys and premium raw materials.
- Demands specialized third-party inspection personnel to audit mill test reports and witness testing.
- Strict hardness caps can limit the mechanical wear resistance of standard valve seating surfaces.
- Complex documentation packages increase engineering administrative overhead during project execution.
High-Pressure Sour Gas Gathering Networks
Upstream production manifolds gather untreated well fluids containing high concentrations of hydrogen sulfide and carbon dioxide. Valve trim components installed in these chokers and ESD valves must undergo rigorous NACE verification to prevent sudden hydrogen embrittlement failure under severe pressure drops.
Amine Sweetening and Acid Gas Recovery Units
Refinery treating units circulate amine solutions loaded with captured hydrogen sulfide and acid gases. Control valves regulating rich and lean amine streams experience accelerated localized turbulence and corrosive attack, necessitating solid nickel alloy valve trim with certified hardness profiles.
Offshore Subsea Production Tree Assemblies
Subsea Christmas trees operate in inaccessible environments where valve replacement requires expensive intervention spreads. Rigorous material verification of internal gate valves and actuation stems guarantees decades of maintenance-free operation under combined hydrostatic and sour wellbore loads.
Crude Oil Stabilization and Desalting Facilities
Midstream pipeline terminals process sour crude oils that release entrained hydrogen sulfide gas during separation stages. Isolation and control valves handling these multi-phase hydrocarbon streams require verified trim materials to prevent sulfide stress cracking during operational upsets.
NACE Material Specifications Table for Valve Trim
Selecting the correct metallic and non-metallic components for sour petroleum service requires strict adherence to ASME B16.34 and ISO 15156 / NACE MR0175 standards. In my experience reviewing material test reports (MTRs) for high-pressure upstream installations, misunderstanding hardness limits is the primary driver of premature sulfide stress cracking (SSC). The engineering data table below outlines the maximum allowable hardness thresholds, acceptable alloy groups, and mandatory metallurgical heat treatments for critical valve trim components operating in severe hydrogen sulfide environments.
Every alloy listed must be verified against certified mill test certificates before machining or assembly occurs in the shop. Pay particular attention to the strict limits imposed on precipitation-hardening stainless steels and cobalt-based hardfacing overlays to prevent catastrophic brittle failure.
| Component | Material Grade | Max Allowable Hardness | Heat Treatment Condition | Primary Code Reference |
|---|---|---|---|---|
| Valve Stem | UNS N07718 (Inconel 718) | 35 HRC Max | Solution Annealed and Aged (Age hardened per NACE) | ISO 15156-3 Table A.2 |
| Valve Ball / Plug | UNS S31803 (2205 Duplex) | 28 HRC Max | Solution Annealed and Quenched (Min 1040 C) | ASME Section II / NACE MR0175 |
| Seat Rings | UNS R30006 (Stellite 6 Overlay) | 35 HRC Equivalent | Plasma Transferred Arc (PTA) Welded & Controlled Cooled | ASTM A217 / NACE MR0175 |
| Body / Bonnet Bolting | ASTM A193 Grade B7M | 22 HRC Max (237 HBW) | Quenched and Tempered (Min tempering temp 650 C) | ASME B16.34 Table 3 |
*Note: Any deviation from the maximum hardness thresholds mandates specialized sour service qualification testing per Annex A of ISO 15156 before equipment release.
Technical Mapping & Specifications Matrix
Establishing complete traceability across valve trim supply chains requires mapping physical components directly to governing standards and material verification protocols. In my professional practice, I utilize this structured entity matrix to align metallurgical test reports with quality control inspection hold points. This systematic approach ensures that every valve trim component deployed in high-pressure sour gas fields complies fully with international regulatory bodies.
The matrix below connects structural acronyms, key testing parameters, and compliance standards into a single unified reference model for project quality managers and piping engineers.
| Entity / Acronym | Full Technical Term | Primary Function & Scope | Governing Code / Standard |
|---|---|---|---|
| MTR | Material Test Report | Certifies chemical composition and mechanical properties of raw heats. | ASTM A370 / EN 10204 3.1 |
| SSC | Sulfide Stress Cracking | Brittle failure mode of high-strength metals under tensile stress in wet H2S. | ISO 15156 / NACE MR0175 |
| PMI | Positive Material Identification | Nondestructive chemical analysis verifying alloy grade prior to assembly. | API 578 / ASME Sec V |
| HRC | Rockwell Hardness C-Scale | Indentation hardness measurement standard for metallic valve trim parts. | ASTM E18 |
*Reference cross-check: All verification entities must be formally signed off by a certified Level III metallurgical inspector during factory acceptance testing.
Site Verification Checklist for NACE Valve Trim
Rigorous site verification prevents non-compliant valve components from entering sour service processing units. When I conduct receiving inspections at fabrication yards, I follow a strict sequential verification protocol to cross-examine physical stamping marks against certified mill test reports and hardness testing gauges.
Use the structured inspection checklist below during pre-installation audits to ensure complete compliance with NACE MR0175 and ASME B16.34 standards.
NACE Material Verification Checklist Items
- MTR Completeness Review: Verify that EN 10204 Type 3.1 mill test certificates match the exact heat numbers stamped on the valve body, bonnet, and internal trim components.
- Positive Material Identification (PMI): Conduct XRF elemental analysis on valve stems, plugs, and seats to confirm alloy percentages for chromium, nickel, and molybdenum.
- Hardness Gauge Calibration: Calibrate portable Leeb or UCI hardness testers against certified test blocks immediately prior to taking physical indentations on valve trim.
- Maximum Hardness Verification: Ensure no tested component exceeds the 22 HRC limit for carbon steels or specific alloy caps outlined in ISO 15156-3.
- Hardfacing Inspection: Check cobalt or nickel-based overlay welds for cracking, porosity, and proper heat treatment condition using penetrant testing (PT).
- Certification Tag Verification: Confirm that a durable stainless steel NACE compliance tag is securely attached to the valve yoke displaying allowable operating limits.
Validation rule: Any discrepancy between physical PMI results and certified mill test reports requires an immediate quarantine of the valve assembly pending metallurgical review.
Field Case Study: Real-World Application
During a major offshore platform commissioning project in the Middle Gulf, our quality engineering team encountered a critical material verification non-conformance on high-pressure production choke valve trim sets.
Field Case Problem
Routine site inspection revealed that a batch of UNS S31803 duplex stainless steel valve plugs exhibited a surface hardness reading of 34 HRC, significantly exceeding the strict 28 HRC maximum threshold mandated by NACE MR0175 / ISO 15156 for sour H2S production service.
- Mill test certificates showed acceptable core hardness but missed localized hardening from improper cold working during final machining.
- Operating conditions included high partial pressures of hydrogen sulfide with trace amounts of wet chlorides, creating a severe risk of sulfide stress cracking.
- Immediate project schedule pressure pushed installation contractors to consider bypassing secondary verification testing.
- Lack of proper hardness gauge calibration logs on site initially cast doubt on the accuracy of the inspection findings.
Field Case Outcome
By strictly enforcing mandatory material verification protocols and rejecting the non-compliant valve trim before well-head integration, our engineering team prevented a catastrophic sour service failure.
- Quarantined all suspect valve assemblies and returned them to the manufacturer for complete solution annealing and controlled re-heat treatment.
- Verified that corrected trim components achieved a stable hardness level of 26 HRC, fully compliant with ISO 15156 requirements.
- Updated site receiving inspection procedures to mandate 100 percent PMI and portable hardness testing on all incoming sour service trim.
- Saved the operating asset millions in potential emergency shutdown costs, environmental fines, and subsea replacement operations.
Engineering Recommendation: Never rely solely on paper mill test reports when procuring safety-critical valve trim for sour environments. Always implement independent verification checks, positive material identification, and hardness testing prior to site installation.
Frequently Asked Engineering Questions
What is the primary objective of NACE MR0175 for valve trim in sour service?
- Restricts maximum allowable hardness values to prevent brittle failure modes.
- Mandates specific heat treatment procedures to control microstructure grain boundaries.
- Aligns with ASME B16.34 pressure boundary requirements.
How do we verify Material Test Certificates against actual valve trim components?
- Cross-check heat numbers stamped on the physical trim against the MTR document.
- Verify chemical composition percentages match ASTM standards for the specific alloy.
- Perform positive material identification (PMI) using XRF guns to confirm alloy grades.
What are the acceptable hardness limits for standard valve trim alloys?
- Carbon and low alloy steels are typically capped at 22 HRC maximum hardness.
- Austenitic stainless steels in solution-annealed condition are generally exempt from strict hardness limits.
- Hardfacing overlays like Stellite require controlled deposition to prevent localized high-hardness zones.
Why is dual certification insufficient without NACE compliance verification?
- Standard manufacturing routes may induce cold work that elevates hardness beyond 22 HRC.
- Heat treatment traceability can be lost during intermediate machining phases.
- Specific NACE MR0175 paragraphs require targeted testing beyond standard ASTM protocols.
How should non-compliant valve trim hardness test results be handled on-site?
- Issue an immediate non-conformance report and segregate the affected batch from active inventory.
- Consult the project metallurgist to determine if specialized re-heat treatment is viable.
- Reject components if re-heat treatment compromises dimensional tolerances or structural integrity.
Field Recommendation
Based on two decades of piping project execution in sour gas processing plants, I advise strict adherence to the following execution protocols for all high-integrity valve trim components:
- If project schedules are tight, never waive independent third-party hardness verification on valve trim components; instead, mandate witness testing at the vendor facility to catch non-compliant lots before shipping.
- If material test certificates lack explicit heat treatment furnace chart recordings, reject the documentation immediately and require the supplier to provide certified thermal cycle graphs before accepting the hardware.
- When dealing with hardfaced overlay components like Stellite, insist on cross-sectional hardness traverses rather than surface-only indentation checks to ensure micro-hardness remains stable through the heat-affected zone.
- Always maintain a dedicated traceability log connecting each physical component tag number directly to its corresponding MTR file and hardness test report for the duration of the plant operating lifecycle.
Complete Course on
Piping Engineering
Check Now
Key Features
- 125+ Hours Content
- 500+ Recorded Lectures
- 20+ Years Exp.
- Lifetime Access
Coverage
- Codes & Standards
- Layouts & Design
- Material Eng.
- Stress Analysis
