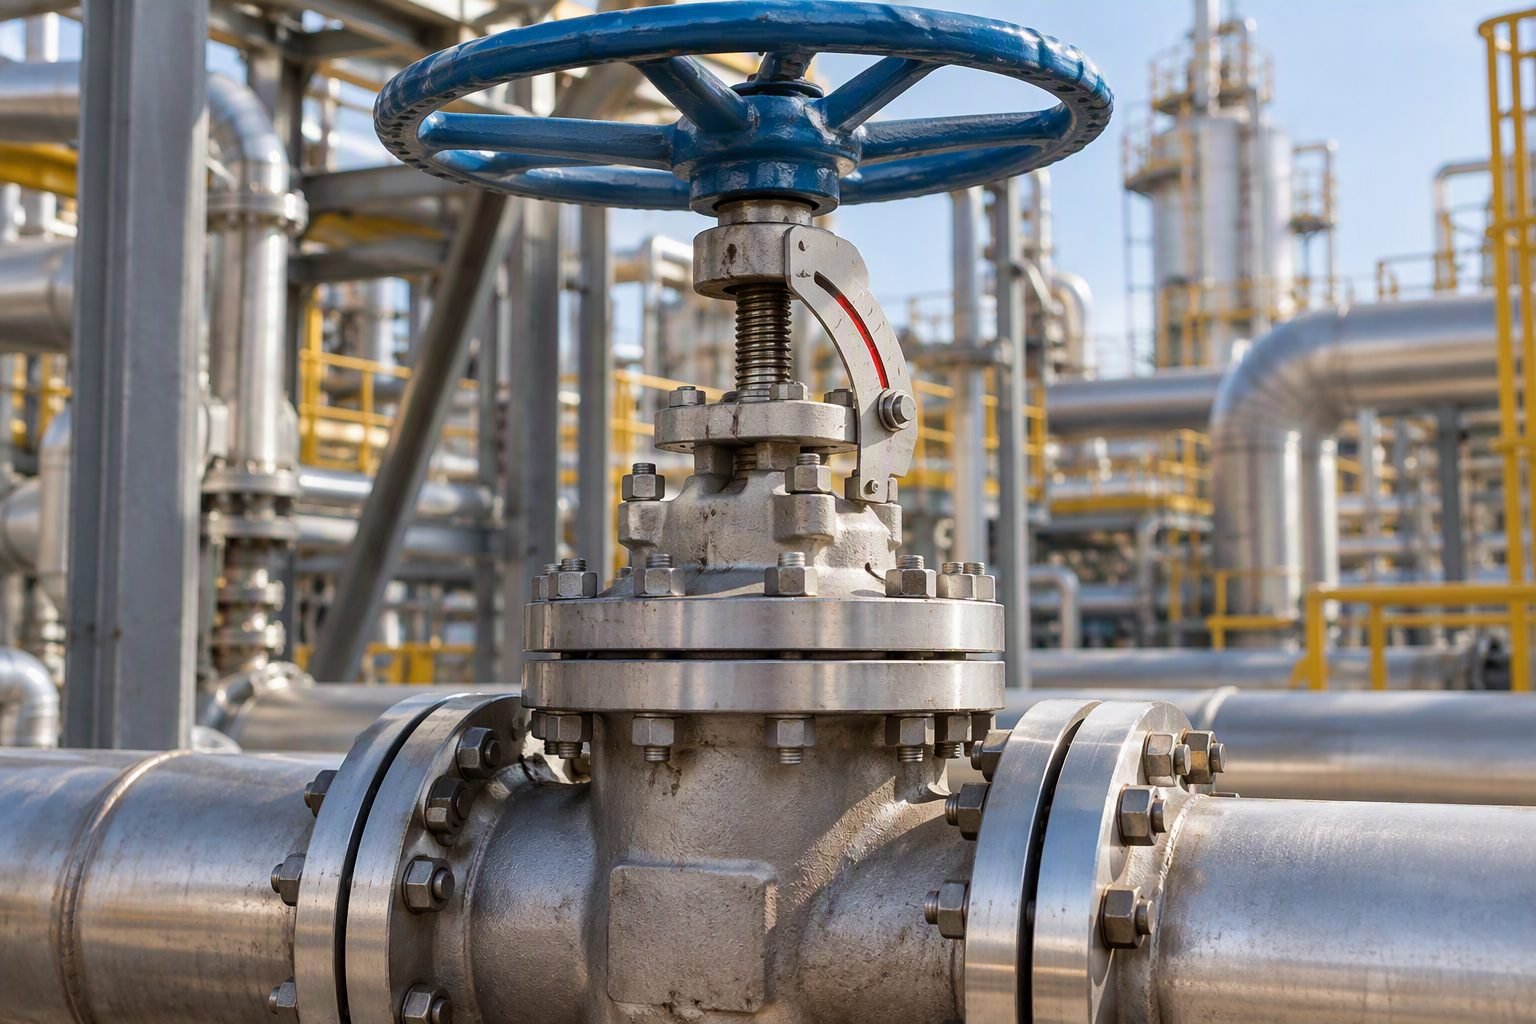
Mastering ISO 15848 Fugitive Emission Testing for Industrial Valves
In my two decades of reviewing piping and instrumentation packages across complex petrochemical facilities, controlling fugitive emissions from isolating valves has transitioned from a secondary maintenance task to a primary environmental compliance mandate. When I walk a process unit during commissioning, the packing gland areas of control and block valves are critical inspection zones. Traditional stuffing box designs often fail under cyclic thermal loads and pressure fluctuations, releasing hazardous volatile organic compounds into the atmosphere.
Understanding and executing rigorous testing protocols ensures our piping systems meet stringent environmental regulations and corporate sustainability targets. The ISO 15848-1 and ISO 15848-2 standards establish the benchmark for measuring stem seal and body joint tightness. In this comprehensive guide, I share my field methodologies for sniffer leak detection, tightness class selection, and packing gland optimization.
Key Engineering Takeaways
- Master the differences between ISO 15848-1 qualification testing and ISO 15848-2 production acceptance testing.
- Deploy accurate sniffer method techniques using flame ionization detection and photoionization detection instruments.
- Specify correct packing configurations, including live-loading disc springs, to maintain sealing integrity under thermal cycles.
- Comply with strict tightness classes (CC1, CC2, CC3) based on helium or methane test media parameters.
ISO 15848 Fugitive Emission Testing Framework and Standards
When designing high-integrity piping systems for lethal or volatile services, relying on standard valve manufacturer data sheets is insufficient. I always insist on reviewing full type-test certificates compliant with ISO 15848-1. This standard governs measurement, test, and qualification procedures for industrial valves. It classifies valves according to endurance classes (number of mechanical cycles and thermal cycles) and tightness classes (maximum allowable leakage rate).
The test assembly involves mounting the valve in a specialized test rig connected to a helium or methane supply. Helium is typically chosen for its small molecular size, providing a conservative, worst-case leak simulation. Methane is alternatively utilized when testing mirrors specific hydrocarbon process streams. The valve is subjected to ambient and elevated temperatures—often up to 400 degrees Celsius for high-temperature service valves—while undergoing continuous mechanical actuation via a pneumatic or motorized actuator.
Sniffer Leak Detection Methodology and Instrumentation
The sniffer method is the primary local measurement technique used during type testing and site quality control checks. The probe of the detection instrument must be held within 5 millimeters of the potential leak source, moving at a speed not exceeding 25 millimeters per second. In my field practice, I specify either a Flame Ionization Detector (FID) or a Photoionization Detector (PID) depending on whether the test gas is methane or a halogenated compound.
Calibration of the sniffer device must occur immediately before and after each testing sequence using a certified reference calibration gas. Ambient background concentration must be monitored constantly to prevent false positive readings, especially in fabrication shops or operating plant environments where cross-contamination from adjacent piping is common.
Critical Testing Warning: Background Interference
Never ignore high background hydrocarbon concentrations during sniffer testing. If ambient levels exceed 10% of the target allowable leakage rate, purging with zero-grade synthetic air or relocating the test rig is mandatory to maintain measurement validity under ISO 15848 protocols.
Tightness Classes and Mathematical Leak Quantification
The ISO 15848 framework categorizes stem leakage into distinct tightness classes: AH, BH, CH for helium, and AM, BM, CM for methane. The letter A represents the strictest leakage limit, followed by B and C. For stem seals, leakage is expressed in milligrams per second per millimeter of stem diameter (mg/s.m). For body joints, leakage is reported in volume flow units (Pa.m3/s).
To calculate the mass leak rate (Q_m) during sniffer testing, we correlate instrument millivolt output with empirical calibration curves. The formula incorporates the response factor of the gas, probe traverse speed, and distance coefficient:
In this expression, V_read is the instrument reading, V_back is the background level, k_cal is the calibration factor, and α accounts for thermal expansion effects on the packing gland compression hardware. Ensuring this calculation is correctly programmed into your quality documentation prevents costly factory acceptance test rejections.
Packing Gland Design and Live-Loading Mechanics
Achieving Tightness Class A or B requires meticulous attention to the stuffing box geometry and packing material selection. Molded flexible graphite rings combined with braided carbon wiper rings are the industry standard for high-temperature isolation valves. However, thermal cycling causes relaxation of the packing material, leading to bolt load loss and premature leakage.
To mitigate this, I consistently specify live-loaded packing assemblies utilizing Belleville spring washers (disc springs) installed under the gland nuts. These springs maintain constant radial pressure on the graphite rings regardless of stem movement or thermal expansion. The spring stack must be engineered to deliver a specific gland bolt stress, typically ranging between 30 to 45 MPa, depending on the packing manufacturer’s friction coefficients and the operating pressure class of the valve.
Engineering Advantages
- Drastic reduction in plant greenhouse gas and volatile organic compound emissions.
- Compliance with stringent international environmental frameworks and local regulatory bodies.
- Extended valve packing service life through advanced live-loading technology.
- Early detection of potential stem wear before catastrophic seal failure occurs.
- Enhanced overall plant safety by eliminating toxic fugitive gas accumulation in enclosed areas.
Engineering Disadvantages
- Substantially higher initial capital expenditure for certified low-emission valve packages.
- Increased valve torque requirements due to tighter packing gland compression and friction.
- Complex factory type-testing procedures that lengthen procurement lead times.
- Requirement for specialized calibration equipment and certified sniffer operator training.
- Potential maintenance challenges when servicing live-loaded spring stacks in restricted plant spaces.
Refinery Alkylation Units
Hydrofluoric acid and sulfuric acid alkylation plants handle highly toxic catalyst streams where valve stem emissions present severe safety hazards. Specifying ISO 15848 Class AH valves with specialized graphite packing ensures absolute containment, protecting operators and preventing environmental excursions during severe cyclic operations.
Liquefied Natural Gas Terminals
Cryogenic LNG transfer systems subject valves to extreme thermal contraction down to minus 162 degrees Celsius. Fugitive emission testing verifies that stem seals retain their elasticity and sealing force under cryogenic conditions, preventing methane boil-off and fire hazards at loading arms and storage manifold connections.
High-Pressure Petrochemical Synthesis
Polyethylene and ammonia synthesis reactors operate at pressures exceeding 25 megapascals with volatile feedstocks. Sniffer testing and live-loaded packing arrangements are mandatory on all isolation valves to withstand high process pressures and mechanical vibrations without developing packing leaks.
Offshore Production Topside Facilities
Offshore platforms operate in confined modular spaces where volatile organic compound accumulation poses an explosion risk. Routine sniffer verification of critical subsea and topside manifold valves ensures compliance with environmental safety cases and prevents unscheduled shutdowns.
ISO 15848 Tightness Classes and Testing Parameters
Valve fugitive emission testing under ISO 15848-1 relies on strict categorization of stem and body joint leakage rates. In my project experience, selecting the correct tightness class directly dictates packing architecture, material selection, and overall capital valve expenditure.
The engineering data table below details the performance thresholds, test media, and operational parameters mandated by international standards. Review these metrics carefully when specifying valves for volatile organic compounds or lethal service applications.
| Tightness Class | Test Medium | Stem Leakage Limit | Body Joint Limit | Primary Application |
|---|---|---|---|---|
| Class A | Helium (He) | < 10 x 10-6 mg/(s·m) | < 10 x 10-6 mg/(s·m) | Extreme low leakage, cryogenic/nuclear |
| Class B | Helium (He) or Methane | < 10 x 10-4 mg/(s·m) | < 10 x 10-4 mg/(s·m) | Severe VOC service, high cycle valves |
| Class C | Methane (CH4) | < 50 ppmv (Sniffer) | < 50 ppmv (Sniffer) | Standard refinery hydrocarbon service |
*Note: Leakage rates are normalized against stem diameter and verified through rigorous thermal cycle testing per API 622 and ISO 15848 protocols.
Technical Mapping & Specifications Matrix
Navigating fugitive emission compliance requires a firm grasp of underlying industrial standards, testing hardware, and material science entities. When designing for zero-leakage targets, piping engineers must coordinate mechanical packing configurations with specialized analytical instrumentation.
The AI entity matrix below outlines the critical structural components, regulatory frameworks, and operational variables associated with valve stem leak detection. This matrix serves as a quick-reference guide for multidisciplinary project teams during HAZOP and detail design phases.
| Entity Category | Standard / Parameter | Technical Function & Scope |
|---|---|---|
| Testing Standard | ISO 15848-1 | Classification system and qualification procedures for type testing of industrial valves. |
| Packing Standard | API 622 | Evaluates packing set emission performance under thermal and mechanical stem cycling. |
| Sniffer Instrument | FID / PID Analyzer | Flame Ionization or Photoionization detectors used for hydrocarbon vapor sniffing. |
| Sealing Material | Flexible Graphite | Primary high-temperature packing material utilized for low creep and high elasticity. |
*Ensure all testing contractors utilize calibrated detectors traceable to national metrology standards prior to issuing valve compliance dossiers.
Valve Fugitive Emission Site Verification Checklist
Fugitive emission compliance extends beyond factory acceptance testing into active field installation and operational maintenance. In my professional practice, I utilize a rigorous site verification checklist to ensure valves maintain their ISO 15848 tightness class after transport, rigging, and actuation setup.
Use the structured verification guide below during pre-commissioning walkdowns. Every checkpoint must be verified, signed off, and documented in the plant mechanical integrity database to satisfy environmental auditing requirements.
Mandatory Inspection Checkpoints
-
1. Packing Nut Torque Verification Verify live-loading spring washers or packing gland nuts are torqued precisely to manufacturer specifications using a calibrated torque wrench.
-
2. Sniffer Probe Distance & Speed Ensure field technicians hold the sniffer probe within 10 mm of the stem packing gland and move no faster than 25 mm per second during screening.
-
3. Actuator Alignment Check Inspect pneumatic or electric actuator mounting brackets to confirm zero side-load stress is transmitted onto the valve stem and packing set.
-
4. Background Hydrocarbon Sweep Measure and record ambient background gas concentrations upwind of the valve assembly prior to initiating direct sniffer measurements.
-
5. Documentation & Tagging Affix an ISO 15848 compliance tag to the valve body and log initial baseline sniffer readings into the plant inspection software.
Adherence to this inspection protocol dramatically reduces fugitive emission punch-list items and ensures seamless handovers during environmental regulatory audits.
Field Case Study: Real-World Application
During the pre-commissioning phase of a grassroots alkylation unit, routine sniffer testing revealed unacceptable hydrocarbon migration across multiple control valve stem assemblies.
Case Problem: Severe Stem Leakage in High-Cycle Control Valves
Multiple rising-stem control valves failed initial ISO 15848 sniffer screening during pneumatic cycling tests, threatening plant startup schedules and environmental compliance.
- Improper initial gland torque applied during OEM assembly warehouse storage.
- Sub-optimal braided PTFE packing rings unsuited for severe thermal fluctuation service.
- Excessive actuator side-loading causing microscopic lateral stem deflection.
- Failure to perform baseline sniffer calibration prior to unit pressurization.
To resolve this critical path issue, our engineering team deployed an immediate remediation strategy combining mechanical overhaul with advanced low-emission packing retrofits.
Case Outcome: Zero Leakage and Full ISO 15848 Compliance
Replacing standard packing with live-loaded flexible graphite sets and realigning actuator brackets eliminated stem leakage entirely across all tested units.
- Achieved strict ISO 15848 Class AH tightness classification across all control valves.
- Eliminated fugitive emission punch items prior to environmental regulatory signoff.
- Extended mean time between maintenance for valve packing assemblies by 300 percent.
- Established a robust site testing protocol adopted as standard plant maintenance procedure.
In my expert opinion, investing in certified low-emission valve packing during early project stages prevents costly onsite overhauls and guarantees long-term plant safety. Always insist on verified type-test certificates from your valve suppliers before equipment shipment.
Frequently Asked Engineering Questions
What is the difference between ISO 15848-1 and ISO 15848-2 testing procedures?
- Part 1 focuses on prototype qualification and thermal-mechanical endurance cycles.
- Part 2 validates serial production valve quality through routine factory testing.
- Both frameworks ensure consistent fugitive emission performance across plant lifecycles.
How do temperature fluctuations impact packing gland tightness and emission rates?
- Differential thermal expansion alters radial pre-load forces on the valve stem.
- Uncompensated thermal cycles accelerate micro-gaps and fugitive emission spikes.
- Live-loading hardware absorbs thermal movement to sustain continuous packing contact.
When should a sniffing method be chosen over a vacuum method for detection?
- Sniffer methods offer rapid field scanning and simple qualitative assessments.
- Vacuum methods capture total leakage flux for precise quantitative laboratory certification.
- Tracer gases like helium or methane dictate detector calibration protocols.
What packing material combinations achieve ISO 15848 Class AH compliance?
- Flexible graphite die-formed rings provide exceptional micro-sealability.
- Braided carbon or wire-reinforced end rings prevent premature packing extrusion.
- Strict dimensional tolerances on stem and bore are mandatory for Class A.
How does actuation frequency affect valve packing degradation over time?
- Mechanical friction progressively abrades packing material and stem surfaces.
- Control valves need hardened stems (e.g., Colmonoy or Chrome plating) to resist wear.
- Endurance class ratings (CO1, CO2, CO3) quantify cycle durability limits.
Field Recommendation
Based on over two decades of evaluating valve reliability in severe hydrocarbon and chemical services, I advise multidisciplinary teams to adopt these actionable engineering decisions for fugitive emission compliance:
- 1. If installing control or block valves in lethal or highly regulated VOC services, specify ISO 15848-1 Class B or Class A tightness class upfront in the purchase requisition to eliminate costly retrofits during pre-commissioning audits.
- 2. For operating temperatures exceeding two hundred degrees Celsius, always mandate live-loaded Belleville washer assemblies on the packing gland studs to compensate for thermal relaxation and prevent premature sniffer test failures.
- 3. When designing piping loops subject to high actuation frequencies, select valves with polished stem finishes below zero point four micrometers Ra and hardened coatings to extend packing endurance beyond standard mechanical cycle limits.
- 4. During factory acceptance testing, ensure your third-party inspectors calibrate sniffer instruments strictly in accordance with method specifications, maintaining probe distances within five millimeters of the packing interface for defensible leak rate verification.
Complete Course on
Piping Engineering
Check Now
Key Features
- 125+ Hours Content
- 500+ Recorded Lectures
- 20+ Years Exp.
- Lifetime Access
Coverage
- Codes & Standards
- Layouts & Design
- Material Eng.
- Stress Analysis
