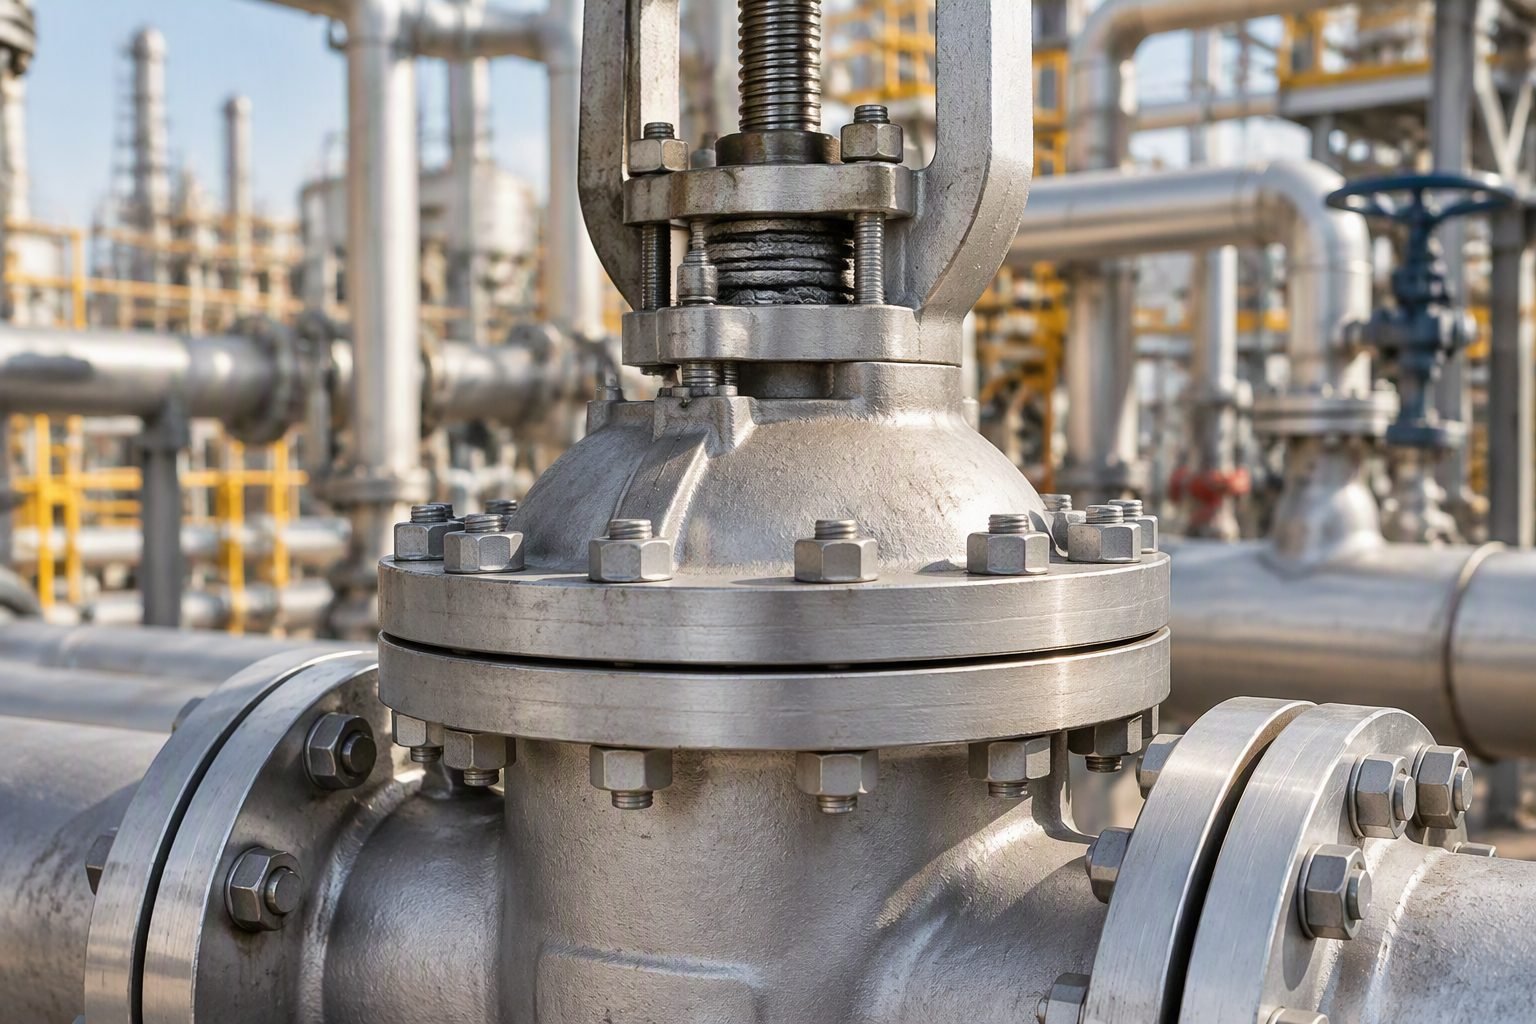
Gate Valve Bonnet Leak Repair Protocols and Engineering standards
In my two decades on site, I have seen too many plant turnarounds stall because operators misdiagnosed a simple stem packing weeping issue as a total catastrophic bonnet gasket failure. When process fluid breaches the pressure boundary of an industrial gate valve, the consequences range from minor fugitive emission fines to severe environmental hazards. Correctly tracing a gate valve bonnet leak requires a methodical diagnostic approach that completely separates fugitive emissions escaping through the packing gland from mechanical joint failures occurring at the primary body-to-bonnet bolted interface.
Understanding the mechanical interaction between the packing rings, live-loading disc springs, and the body-to-bonnet stud preload is non-negotiable for piping reliability engineers. Throughout this guide, I will walk you through the rigorous engineering diagnostics mandated by API 622 and API 624. You will learn precise torque calculation methods, gasket seating stress requirements, and field-proven remediation sequences designed to achieve zero-leakage compliance without forcing premature valve unbolting.
Key Engineering Takeaways:
- Isolate stem packing emissions from gasket failures before initiating any hot-bolting procedures.
- Apply strict ASME PCC-1 controlled bolting practices for all high-pressure bonnet flange repairs.
- Utilize API 622 certified low-emission graphite packing sets to maintain environmental compliance.
Engineering Diagnostics for Gate Valve Bonnet Leak Scenarios
Diagnostic isolation methodology: The precise engineering practice of differentiating stem packing fugitive emissions from body-bonnet gasket failures utilizing localized sniffer testing, thermal imaging, and pressure boundary analysis per API 591 guidelines.
When investigating a gate valve bonnet leak, rushing to tighten the exterior bolting is a dangerous mistake. In my experience, tightening bonnet studs when the actual leak path is a degraded graphite packing ring only masks the symptom while transferring stress to the yoke arms. A systematic engineering audit must begin with verifying the exact geographical origin of the fluid path. The stem packing box houses braided flexible graphite rings compressed by a gland follower and stud bolts, whereas the bonnet joint relies on a confined or unconfined metallic or spiral-wound gasket compressed between precision-machined mating faces.
To perform an accurate diagnosis, maintenance personnel must utilize Method 21 portable hydrocarbon detectors or localized bubble testing while the valve is pressurized under normal operating conditions. If the vapor concentration spikes immediately around the stem periphery and above the packing flange, the root cause is localized packing wear, thermal relaxation, or insufficient gland nut torque. Conversely, if hydrocarbons or steam condensate pool directly on the outer diameter of the bonnet flange ledge, the primary spiral-wound or ring-joint gasket has suffered mechanical relaxation, over-pressure blowout, or flange face corrosion.
CRITICAL ENGINEERING WARNING: Hot Bolting Limitations
Never attempt to hot-bolt a leaking body-bonnet joint on hydrocarbon or high-pressure steam service exceeding 300°C without a formal engineering stress review. Relaxing or retightening bonnet studs on a degraded gasket under full operating pressure can cause catastrophic gasket blowout, resulting in massive toxic or flammable releases. Always depressurize and purge the valve cavity per plant safety procedures before altering bonnet stud torque.
Stem Packing Mechanics and API 622 Compliance
The stem packing box is engineered to restrict fluid migration along the reciprocating and rotating gate valve stem. Under API 622 standards, packing materials must withstand severe thermal cycling while maintaining fugitive emission levels below 100 ppm total hydrocarbon. Standard flexible graphite rings require a minimum specific radial stress to deform and seal against the stuffing box wall and the stem surface. When thermal gradients cause differential expansion between the austenitic stainless steel stem and the carbon steel bonnet, the packing loses its initial elastic memory, resulting in fugitive leaks.
To combat thermal relaxation, modern industrial gate valves utilize live-loading assemblies comprising Belleville disc spring washers stacked in series or parallel beneath the gland nut nuts. These springs provide continuous axial displacement compensation, maintaining consistent packing stress despite thermal expansion cycles. When calculating required gland bolt torque, engineers must factor in the friction coefficient of the specific thread lubricant and the required radial seating stress, typically ranging between 25 MPa and 40 MPa for flexible graphite ring sets.
Bonnet Flange Gasket Mechanics and Bolting Stress
The structural integrity of the body-to-bonnet joint depends entirely on maintaining uniform bolt preload across all studs. According to ASME BPVC Section VIII Division 1 and ASME PCC-1, the assembly bolt stress must be sufficient to crush the gasket into the flange seating grooves and maintain hydrostatic end-load resistance without exceeding the yield strength of the stud material (typically ASTM A193 Gr. B7).
When a gate valve bonnet leak occurs at this flanged interface, it is frequently caused by uneven bolt torquing during initial installation or uneven thermal growth during startup. Using calibrated hydraulic tensioners or electronic torque wrenches with a strict star-pattern tightening sequence is mandatory. The target bolt stress must achieve the minimum gasket seating stress (y) and operating stress factor (m) outlined in ASME Div 1 Appendix 2. If the gasket has undergone creep relaxation or chemical degradation due to process fluid incompatibility, retightening will fail, necessitating a complete bonnet disassembly, flange face inspection, and gasket replacement.
Bonnet Joint Failure Root Cause Analysis Steps
- 1. Perform ultrasonic thickness testing (UT) on the bonnet wall to rule out internal erosion-corrosion.
- 2. Inspect stud threads for galling, corrosion pitting, and thread elongation exceeding 104% of nominal length.
- 3. Verify flange face parallelism and radial runout using laser alignment or precision feeler gauges.
- 4. Examine removed gasket remnants for inward buckling, over-compression, or localized chemical attack.
Repair strategy comparison: Evaluating live-loading retrofits versus full bonnet gasket replacements based on downtime, fugitive emission reduction, and long-term mechanical reliability.
Advantages
- ✓ Live-loading retrofits: Eliminates frequent manual packing adjustments by compensating automatically for thermal expansion and mechanical wear.
- ✓ API 622 compliance: Low-emission graphite packing sets achieve fugitive emissions consistently below stringent EPA Method 21 limits.
- ✓ Controlled bolting: Adhering to ASME PCC-1 procedures prevents flange distortion and extends gasket operational lifespan.
- ✓ Targeted isolation: Differentiating stem leaks from bonnet leaks prevents unnecessary and costly valve teardowns.
Disadvantages
- ✗ High initial retrofit cost: Installing Belleville spring assemblies and precision low-emission packing increases material expenses.
- ✗ Operational downtime: Full bonnet gasket replacement requires complete line depressurization, purging, and valve unbolting.
- ✗ Space constraints: Retrofitting live-loading springs on tight multi-valve manifolds can interfere with thermal insulation cladding.
- ✗ Skilled labor dependency: Requires certified technicians trained in controlled torque calculation and flange parallelism measurement.
Industrial deployment contexts: Practical engineering implementations of gate valve bonnet leak tracing and repair protocols across high-severity processing environments.
Refinery Hydrocracker Unit Isolation Valves
High-pressure hydroprocessing units operate with severe hydrogen-rich hydrocarbon streams at elevated temperatures. Tracing gate valve bonnet leaks here requires specialized sniffing tools to detect microscopic hydrogen migration through spiral-wound bonnet gaskets before hydrogen embrittlement compromises the surrounding bolting matrix.
Supercritical Power Plant Main Steam Lines
Main steam isolation gate valves experience extreme thermal shock during startup and shutdown cycles. Engineers apply live-loaded flexible graphite stem packing and Kammprofile bonnet gaskets to prevent steam cutting across the flange face, ensuring continuous compliance with emission mandates.
Petrochemical Cryogenic Ethylene Storage
Low-temperature ethylene handling causes material contraction and severe seal hardening. Bonnet leak tracing in cryogenic service utilizes acoustic emission monitoring to identify internal gasket relaxation caused by extreme thermal shrinkage down to -104°C.
Offshore Upstream Production Manifolds
Platform topside gate valves are subject to corrosive marine atmospheres and high vibration. Preventive maintenance routines incorporate ultrasonic bolt load verification to ensure bonnet integrity remains intact despite continuous wave-induced structural flexing.
Acid Gas and Sour Water Stripping Units
Handling hydrogen sulfide and sour water requires strict adherence to NACE MR0175 material standards. Bonnet leak investigations in sour service prioritize rapid fugitive emission containment to protect operating personnel from highly toxic H2S accumulation in confined pipe racks.
In my twenty years of managing high-pressure piping systems, I have seen many field technicians misdiagnose a bonnet-to-body joint leak as a simple stem packing failure. This error leads to unnecessary packing adjustments that can damage the valve stem or cause actuator binding. To prevent these costly mistakes, we must analyze the distinct physical characteristics and operating limits of each leak path.
The table below provides a direct engineering comparison between stem packing and bonnet bolted joint assemblies. It outlines the governing design standards, typical leak mechanisms, and the corrective torque strategies required to restore a zero-leakage seal under pressure.
| Parameter | Stem Packing Gland | Bonnet-to-Body Bolted Joint |
|---|---|---|
| Governing Standard | API 622 / API 600 | ASME B16.34 / ASME PCC-1 |
| Primary Leak Mechanism | Friction wear, packing consolidation, stem scoring | Thermal cycling, bolt relaxation, gasket degradation |
| Diagnostic Method | Visual trace along stem, fugitive emissions sniffing | Bubble test, thermal imaging, flange gap measurement |
| Corrective Action | Gland nut adjustment, packing consolidation rings | Controlled hot torqueing, gasket replacement |
| Torque Control Method | Target gland bolt torque (inch-pounds) | Star-pattern hydraulic tensioning (foot-pounds) |
Applying the correct torque profile is the most reliable way to stop a packing leak without seizing the stem. Always refer to the manufacturer’s torque limits before adjusting gland bolts to avoid crushing the graphite rings.
To execute a successful repair on a leaking gate valve, you must understand the precise relationship between the physical components, their material specifications, and the governing industry codes. Each element of the bonnet assembly operates under specific mechanical constraints that dictate how it responds to thermal cycling and pressure surges.
This technical mapping matrix connects key valve components with their corresponding material standards, critical design parameters, and the exact codes that govern their performance. Use this matrix to verify that replacement parts and repair procedures comply with the original design basis of your piping system.
| Component Entity | Acronym | Material Specification | Critical Parameter | Governing Standard |
|---|---|---|---|---|
| Stem Packing Ring | SPR | Flexible Graphite with Corrosion Inhibitor | Fugitive Emissions < 100 ppm | API 622 |
| Bonnet Gasket | BG | Spiral Wound SS316 with Graphite Fill | Minimum Gasket Seating Stress | ASME B16.20 |
| Gland Studs & Nuts | GSN | ASTM A193 Gr. B7 / ASTM A194 Gr. 2H | Yield Strength & Thread Pitch | ASME B16.34 |
| Bonnet Bolting | BB | ASTM A193 Gr. B7 (High Temp Carbon Steel) | Target Bolt Tension & Elongation | ASME PCC-1 |
In my experience, using mismatched materials during a shutdown is a primary cause of premature joint failure. This matrix serves as a quick-reference guide for engineering teams to cross-reference component specifications during the planning phase of a turnaround.
Site Leak Verification: A systematic field inspection protocol designed to isolate, identify, and document gate valve bonnet and stem packing leaks prior to executing mechanical adjustments or hot torqueing.
Before any technician touches a wrench to a leaking valve under pressure, a rigorous safety and technical assessment must be completed. Working on live, pressurized systems carries inherent risks of sudden gasket blowout or stem ejection. I always insist on a formal verification process to ensure the team has identified the exact leak source and verified the system operating conditions.
In my experience, hasty field adjustments without proper verification often worsen the leak. A minor packing weep can quickly escalate into a catastrophic steam or hydrocarbon release if the gland studs are corroded or over-stressed. This protocol ensures that we establish a safe working boundary and gather accurate diagnostic data before initiating any repair work.
- Verify system pressure and temperature are within safe limits for live adjustment.
- Clean the bonnet and gland area using a non-corrosive wire brush to clear debris.
- Apply a certified leak detection fluid to differentiate between packing blow-by and gasket bypass.
- Check the gland follower for parallelism; uneven gland loading causes localized packing wear.
- Inspect stem surfaces for pitting, scoring, or corrosion that could shred new packing rings.
- Confirm that the bonnet bolting material matches the piping specification before applying torque.
- Verify that the packing gland has remaining travel; if bottomed out, packing replacement is required.
- Measure and record the current bolt elongation or torque values using calibrated tools.
- Ensure a standby safety watch and appropriate personal protective equipment (PPE) are in place for hazardous fluids.
If the leak persists after executing these checks and performing a controlled torque adjustment, the valve must be scheduled for isolation and a complete gasket or packing replacement. Never attempt to over-torque bolts beyond the maximum limits specified in ASME PCC-1.
Field Case Study: Real-World Application
The Problem:
During a winter startup at a major petrochemical refinery, a 12-inch Class 600 gate valve handling high-pressure superheated steam began leaking heavily from the bonnet area. The initial field report identified the leak as a simple stem packing failure, and the maintenance crew prepared to tighten the gland. However, upon closer inspection, I noticed that the steam was actually escaping from the backside of the bonnet flange, indicating a gasket failure rather than a packing leak. The steam plume was blowing directly onto the actuator, risking electrical failure of the limit switches. Tightening the packing gland under these conditions would have done nothing to stop the leak and would have likely seized the stem, compounding the operational emergency.
Root causes of this specific field failure included:
- Rapid thermal cycling during the startup sequence which caused differential expansion.
- Uneven initial torque application on the bonnet bolts during the previous turnaround.
- Use of a non-conforming, low-density graphite gasket that lacked a metal reinforcement ring.
- Relaxation of the ASTM A193 Grade B7 bonnet studs due to prolonged high-temperature service.
The Outcome:
We immediately halted the packing adjustment and implemented a controlled hot-torque procedure on the bonnet-to-body bolted joint following ASME PCC-1 guidelines. By using a calibrated hydraulic torque wrench, we applied torque in 30% increments using a cross-pattern star sequence. This restored uniform gasket seating stress without over-stressing the individual studs. This action successfully isolated the leak path and allowed the plant to remain online until the next scheduled maintenance window.
Measurable results and technical outcomes included:
- Achieved complete, zero-leakage isolation of the steam path within two hours of detection.
- Prevented an unscheduled plant shutdown, saving an estimated 180,000 in lost production.
- Replaced the temporary gasket with an API 622 compliant spiral-wound gasket during the next outage.
- Implemented a mandatory hydraulic tensioning protocol for all Class 600 and higher bonnet joints.
My direct recommendation for high-temperature steam systems is to always perform a thermal-cycle torque check on bonnet bolting during startup. Never assume a leak near the yoke is packing-related without conducting a thorough visual and thermal imaging trace.
Frequently Asked Engineering Questions
How do you distinguish between a stem packing leak and a bonnet gasket leak?
- Wipe the area dry and apply a developer powder to trace the exact fluid path.
- Check the gland follower tilt; an uneven gland often forces fluid up one side of the stem.
- Inspect the bonnet joint perimeter for localized steam cuts or product crystallization.
What are the testing requirements for low-emission packing under API 622?
- The packing must maintain leakage below 100 parts per million (ppm) without adjustment.
- It evaluates weight loss, corrosion tendencies, and high-temperature stability.
- Specifying API 622 certified packing is standard practice for volatile organic compounds (VOCs).
Can you tighten a gate valve bonnet joint while the piping system is online?
- Isolate and depressurize the line completely before attempting any bolt adjustments.
- Verify the torque values against the original design specifications using a calibrated wrench.
- Replacing the gasket is the only permanent solution if torque adjustments fail.
Why does graphite packing require sacrificial zinc active corrosion inhibitors?
- Inhibitors act as sacrificial anodes to protect the stem from pitting.
- Pitted stems create micro-voids that destroy new packing rings during operation.
- Ensure your packing specification complies with ASME B16.34 material requirements.
What is the correct torque pattern for a bolted gate valve bonnet?
- Apply torque in increments of 30%, 60%, and 100% of the target value.
- Perform a final circular pass at 100% torque to verify uniformity.
- Uneven loading causes localized gasket crushing and subsequent joint failure.
How does API 600 govern the design of the stem packing chamber?
- It requires a minimum number of packing rings combined with a lantern ring if specified.
- The standard mandates a smooth stem finish to minimize packing wear during cycling.
- It ensures the backseat design allows temporary isolation for packing maintenance.
Field Recommendation
Valve Repair Decisions: Executing targeted maintenance on gate valve bonnets requires a systematic evaluation of operating conditions, gasket materials, and emission standards to prevent recurring failures.
- If you encounter a persistent stem leak on a high-cycle hydrocarbon valve, I recommend upgrading to an API 622-approved die-formed graphite packing set with carbon fiber corner rings because this configuration resists extrusion and maintains a tight seal under thermal cycling.
- When dealing with a leaking bonnet joint on a class 600 or higher valve, do not attempt to simply over-torque the existing bolts; instead, schedule an immediate shutdown to replace the gasket with a spiral-wound metallic gasket containing an inner ring to prevent radial buckling.
- In my experience, if the valve stem shows any signs of pitting or scoring deeper than 0.2 millimeters, you must replace the stem entirely rather than repack it, as the rough surface will shred new packing rings within a few dozen strokes.
- If your facility operates under strict fugitive emission regulations, choose live-loaded packing systems with Belleville spring washers because they automatically compensate for packing relaxation and thermal expansion without manual intervention.
Complete Course on
Piping Engineering
Check Now
Key Features
- 125+ Hours Content
- 500+ Recorded Lectures
- 20+ Years Exp.
- Lifetime Access
Coverage
- Codes & Standards
- Layouts & Design
- Material Eng.
- Stress Analysis
