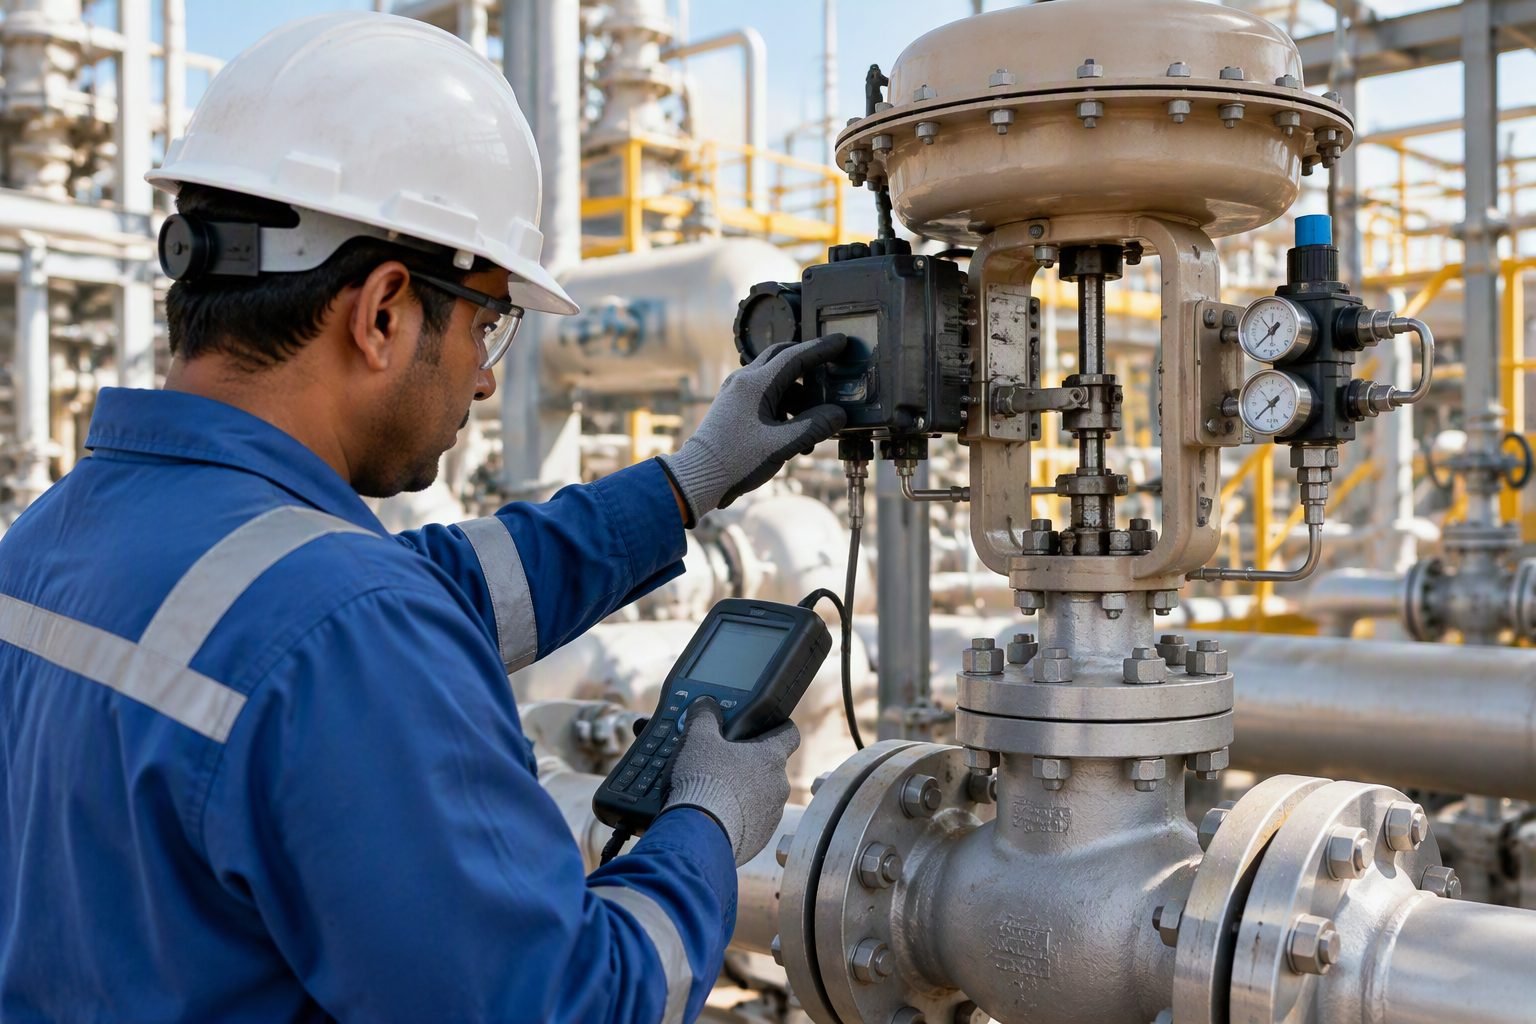
Control Valve Trim Rangeability Verification in Industrial Piping
In my two decades of commissioning major hydrocarbon processing units, I have frequently witnessed plant upsets caused by a simple yet insidious oversight: assuming a control valve will perform precisely as its manufacturer catalog data predicts in the field. When a technician stands beside a high-pressure drop letdown station with a handheld HART communicator, adjusting a digital valve positioner, the ultimate goal is verifying that the physical trim rangeability matches design expectations.
Control valve trim rangeability dictates the turndown ratio—the span between the maximum controllable flow and the minimum controllable flow where the valve can still exert meaningful throttling authority. If your actual operating conditions deviate from design parameters or if seat leakage and mechanical hysteresis creep in, your process control loops will begin to oscillate, leading to accelerated mechanical wear and lost production.
Key Engineering Takeaways
- Catalog rangeability numbers represent ideal laboratory conditions under single-phase water flow.
- Field calibration using smart communicators isolates positioner feedback errors from mechanical trim wear.
- Low-end throttling instability occurs rapidly if the installed flow characteristic deviates from the inherent characteristic.
- Complying with ASME B16.104 leakage classes helps preserve lower-range stability over time.
Mastering Control Valve Trim Rangeability Calculations and Field Testing
When designing industrial piping networks, engineers specify control valves based on the valve flow coefficient, commonly denoted as Cv. The inherent rangeability of a trim style—such as a contoured plug, characterized cage, or V-notch ball—defines the ratio of maximum Cv to minimum controllable Cv. For a standard equal percentage globe valve, this catalog ratio is typically 50:1 or greater. However, the installed rangeability is almost always lower due to system pressure drop distribution.
To calculate installed rangeability, we must examine the valve pressure drop ratio, known as factor P. When a piping system has significant friction losses in adjacent piping, headers, and fittings, the pressure drop across the valve decreases as flow increases. This dynamic causes the installed flow characteristic to warp away from the inherent characteristic, severely compressing the controllable flow range at the high end.
Mathematical Verification of Installed Cv
The sizing equations established by IEC 60534-2-1 govern how we convert process mass flow rates into required Cv values. For liquid service, the sizing equation is expressed as:
Where Q represents volumetric flow rate in US gpm, SG is specific gravity relative to water at 60 degrees Fahrenheit, and Delta-P is the effective pressure drop across the valve trim in psi under flowing conditions. During field verification, a technician must record the actual upstream and downstream gauge pressures while stepping the valve positioner through 0%, 10%, 20%, up to 100% stroke.
Hysteresis, Dead Band, and Positioner Tuning
Mechanical friction in packing boxes and guide bushings introduces hysteresis, which directly degrades low-end rangeability. If a digital positioner has an aggregate dead band exceeding 0.5% of span, the valve will exhibit limit cycling when the controller attempts micro-adjustments near the closed position.
During my site commissioning work, I mandate a complete bench set and stroke calibration before hookup to the process. Using a handheld communicator, the technician checks the travel sensor feedback against the 4-20mA or digital HART command signal. Any deviation greater than 0.25% requires an automatic zero and span recalibration routine within the positioner firmware.
Critical Safety Warning on High-Pressure Drop Trims
Never stroke a high-pressure letdown valve through its minimum position during initial dry loop checks without verifying that upstream block valves are positively isolated. High velocity jetting across partially open micro-trims can induce severe acoustic vibration, structural fatigue, and catastrophic trim erosion within minutes, violating API 553 installation safety guidelines.
Evaluating Cavitation and Flashing Impacts
Trim rangeability is further constrained when operating near vapor pressure limits. If liquid pressure falls below the vapor pressure at the vena contracta, vapor bubbles form and subsequently collapse violently against the trim metal. This cavitation pitting alters the smooth profile of the cage windows, destroying the precise flow area ratio required for low-end throttling stability.
Field technicians must cross-reference handheld diagnostic traces with calculated cavitation index values (σ). If the operating sigma drops below the critical cavitation threshold (σ_c), multi-stage anti-cavitation trim must be retrofitted, or the operational pressure drop must be redistributed across downstream restriction orifices.
Advantages & Disadvantages
Engineering Advantages
- Eliminates low-end process hunting and loop oscillation by confirming real-world turndown.
- Validates digital positioner feedback against mechanical stem travel with high precision.
- Identifies packing box friction and dead band issues before they escalate into sticking failures.
- Ensures compliance with stringent fugitive emission and leakage standards like ASME B16.104.
- Optimizes pump head requirements by preventing oversized valves from operating on the extreme lower stem positions.
Engineering Disadvantages
- Requires temporary process interruption or bypass operation to safely measure differential pressure across extremes.
- Handheld communicator diagnostic procedures demand specialized technician training and certification.
- High initial setup time for recording complete signature curves on large multi-stage control valves.
- Software configuration discrepancies between HART, Foundation Fieldbus, and Profibus protocols can complicate logging.
- Environmental exposure in extreme weather plants can degrade local pressure gauge accuracy over time.
Real-World Applications
Refinery Hydrocracker Letdown Stations
High-pressure reactor effluent letdown valves handle severe flashing services where accurate trim rangeability is vital. Technicians use handheld communicators during turnaround inspections to verify that micro-channel cages maintain their turndown capability against erosive catalyst fines.
Cryogenic Liquefied Natural Gas Processing
In LNG liquefaction trains, Joule-Thomson expansion valves operate at extreme low temperatures where metal contraction alters seating clearances. Field verification ensures that thermal shrinkage does not bind the valve trim, preserving the 50:1 turndown required for precise temperature control.
Boiler Feedwater High-Pressure Regulation
Power plant feedwater systems rely on multi-stage anti-cavitation control valves to regulate drum levels across wide load swings from startup to full capacity. Calibrating the digital positioner stroke via smart communicators prevents thermal shock and water hammer during low-flow transient conditions.
Petrochemical Catalyst Addition Skids
Precise dosing of liquid catalyst relies on micro-flow control valves operating near the lower boundary of their rangeability curve. Field diagnostic tools verify that dead band and hysteresis remain within tight tolerances to prevent erratic reactor conversion rates.
Engineering Data Table: Control Valve Trim Characteristics and Verification Parameters
Understanding the quantitative relationship between valve travel and flow capacity requires precise engineering data. When evaluating control valve trim rangeability, instrumentation and piping engineers must analyze how different characteristic curves behave under actual process conditions. In my field experience, discrepancies between theoretical catalog turndown and verified in-situ performance often stem from uncompensated pressure drop ratios or piping geometry effects near the valve inlet.
The data matrix below outlines standard trim types governed by ASME and ISA standards, correlating nominal rangeability values with expected turndown limits and typical industrial process applications. Review these parameters carefully when establishing baseline calibration targets for smart positioners.
| Trim Characteristic | Catalog Rangeability | Effective Field Turndown | Primary Application Range | Governing Standard |
|---|---|---|---|---|
| Linear Trim | 30:1 to 50:1 | 25:1 to 35:1 | Liquid level control & constant pressure drop loops | ASME B16.104 |
| Equal Percentage | 50:1 to 100:1 | 40:1 to 75:1 | Temperature control & high pressure drop variation | ISA-75.11.01 |
| Quick Opening | 10:1 to 15:1 | 8:1 to 12:1 | On-off emergency shutdown & pressure relief bypass | ASME B16.34 |
| Modified Parabolic | 30:1 to 50:1 | 20:1 to 40:1 | Moderate flow modulation with non-linear loads | ISA-75.01.01 |
Note: Effective field turndown values reflect typical installation degradation caused by reducer geometry, piping friction losses, and positioner deadband accumulation.
Technical Mapping & Specifications Matrix
Complex process instrumentation frameworks require meticulous mapping of physical entities, regulatory acronyms, and diagnostic parameters. When commissioning automated piping loops, engineers must synchronize digital HART protocols with mechanical valve signatures to ensure compliance with international industrial standards.
The entity specification matrix below breaks down the core hardware, software, and procedural components governing loop verification. Each entry cross-references recognized engineering bodies such as IEC and ASME to maintain strict quality assurance during plant turnarounds.
| Entity Term / Acronym | Classification | Operational Parameter | Governing Standard Reference |
|---|---|---|---|
| HART Communicator | Diagnostic Handheld Tool | 4-20mA signal trimming & stroke calibration | FieldComm Group HART Protocol |
| Valve Positioner | Electro-Pneumatic Device | Closed-loop travel feedback & air pressure modulation | IEC 60534-6-1 |
| Valve Trim (Plug & Seat) | Internal Wetted Hardware | Flow characterization and rangeability determination | ASME B16.34 |
| Pressure Gauge Assembly | In-Line Monitoring Sensor | Supply pressure verification & differential drop check | ASME B40.100 |
Reference this entity matrix alongside piping and instrumentation diagrams during pre-commissioning walkthroughs to verify component compatibility.
Site Verification Checklist: Control Valve Trim Rangeability Inspection
Executing a methodical site verification process is essential before declaring any control loop ready for service. When I perform field audits on high-pressure throttling valves, I rely on a structured verification sequence to catch mechanical binding, hysteresis, and signal calibration errors early.
Review and execute each validation rule in the checklist below to confirm that actual operating trim rangeability aligns with certified manufacturer data sheets and ASME design specifications.
Mandatory Field Inspection Checkpoints
-
1. Physical Trim Inspection: Verify that installed valve plug and seat contours match the data sheet characteristic curve (Linear, Equal Percentage) per ASME B16.34.
-
2. Handheld Communicator Connection: Hook up the HART communicator to the positioner terminals, ensuring clean signal communication without voltage drop across the loop.
-
3. Zero and Span Calibration: Calibrate the 0% and 100% travel points using the positioner auto-stroke routine, confirming mechanical feedback linkage is tight.
-
4. Supply Pressure Verification: Check local pressure gauges upstream and downstream of the valve body to verify that operating differential pressure matches design calculations.
-
5. Deadband and Hysteresis Testing: Step the signal input up and down in 10% increments to record travel response and ensure hysteresis remains below 1.0% of span.
-
6. Low-Flow Rangeability Audit: Observe valve behavior in the 0% to 15% opening range to verify that the seating surface avoids wire-drawing and maintains stable flow modulation.
Completing this verification protocol guarantees that the installed hardware will perform reliably under dynamic process loads, minimizing premature trim wear and costly unscheduled downtime.
Field Case Study: Real-World Application
Real-world commissioning challenges frequently expose discrepancies between theoretical valve sizing sheets and actual plant behavior. During a recent refinery expansion project involving high-pressure boiler feed water control, our instrumentation team encountered severe process oscillation during low-load operations, prompting an immediate investigation into the valve trim rangeability.
Field Problem Identification
The 4-inch equal percentage control valve exhibited erratic flow control and process instability whenever plant throughput dropped below 20 percent of design capacity.
- Actual field turndown measured approximately 18:1, falling far short of the manufacturer catalog rating of 50:1.
- The handheld communicator revealed that the digital positioner feedback linkage had developed micro-slippage during thermal cycling.
- Local pressure gauges indicated excessive pressure drop across upstream reducer fittings, creating localized turbulence before the fluid entered the valve body.
- The control loop tuning parameters were constantly hunting because the effective trim range was compressed at the lower end of travel.
Field Resolution & Engineering Outcome
Systematic recalibration and mechanical adjustments successfully restored full operational span and eliminated process hunting across all operating regimes.
- Re-secured and pinned the positioner feedback arm, reducing mechanical deadband to less than 0.3 percent of full stroke.
- Performed a complete digital re-ranging via the HART communicator, aligning 4-20mA signal inputs precisely with physical valve plug movement.
- Installed straight pipe spool pieces upstream to eliminate turbulence, stabilizing the inlet pressure profile per ASME piping guidelines.
- Achieved a verified field rangeability of 42:1, ensuring stable temperature control and preventing premature seat erosion.
This case underscores the critical importance of hands-on field verification. Relying solely on factory calibration sheets without verifying in-situ positioner response and pressure drop profiles invites process instability and premature equipment failure.
Frequently Asked Engineering Questions
What is control valve trim rangeability and why does it matter in industrial piping?
- Defines the usable turndown ratio defined by ISA-75.01.01 standards.
- Prevents low-flow instability and seat damage during minimum process demand.
- Ensures steady-state loop tuning remains valid across wide operating envelopes.
How does a handheld communicator verify valve trim performance in the field?
- Executes automated travel sensor calibration across zero and span points.
- Diagnoses deadband and hysteresis in the pneumatic actuator assembly.
- Compares actual stem position against controller output signals in real time.
What causes actual trim rangeability to deviate from manufacturer catalog data?
- High pressure drop ratios induce fluid flashing or cavitation at low openings.
- Piping geometry and upstream elbows create distorted inlet velocity profiles.
- Mechanical wear on the plug and seat alters inherent flow characteristics.
Which standards govern control valve sizing and performance verification testing?
- IEC 60534 dictates industrial-process control valve capacity equations.
- ASME B16.104 establishes seat leakage class tolerances across various trim designs.
- ISA-75 guidelines cover practical sizing and installation verification procedures.
How do you troubleshoot valve chatter and poor low-flow stability in the field?
- Review actual process flow rates against calculated valve sizing curves.
- Adjust positioner tuning parameters and PID controller gain settings.
- Inspect trim for cavitation damage or replace with characterized low-flow plugs.
Field Recommendation
- If initial commissioning reveals severe flow oscillation at low process demands, do not alter PID tuning parameters immediately; instead, connect a handheld communicator to verify that the valve positioner’s low-signal characterization curve matches the installed trim geometry.
- When reviewing piping layouts for high-pressure letdown services, insist on installing upstream straight runs of at least 15 pipe diameters to eliminate inlet swirl, which severely degrades catalog rangeability and causes premature trim erosion.
- For severe service applications involving flashing fluids, choose hardened Stellite or ceramic-coated multi-stage trim options rather than standard equal-percentage plugs to preserve accurate rangeability and prevent catastrophic seat degradation during turndown.
- During scheduled turnaround events, mandate a complete stroke signature test via smart positioner diagnostics rather than a simple visual stroke check to catch early mechanical hysteresis before it compromises loop performance.
Complete Course on
Piping Engineering
Check Now
Key Features
- 125+ Hours Content
- 500+ Recorded Lectures
- 20+ Years Exp.
- Lifetime Access
Coverage
- Codes & Standards
- Layouts & Design
- Material Eng.
- Stress Analysis
