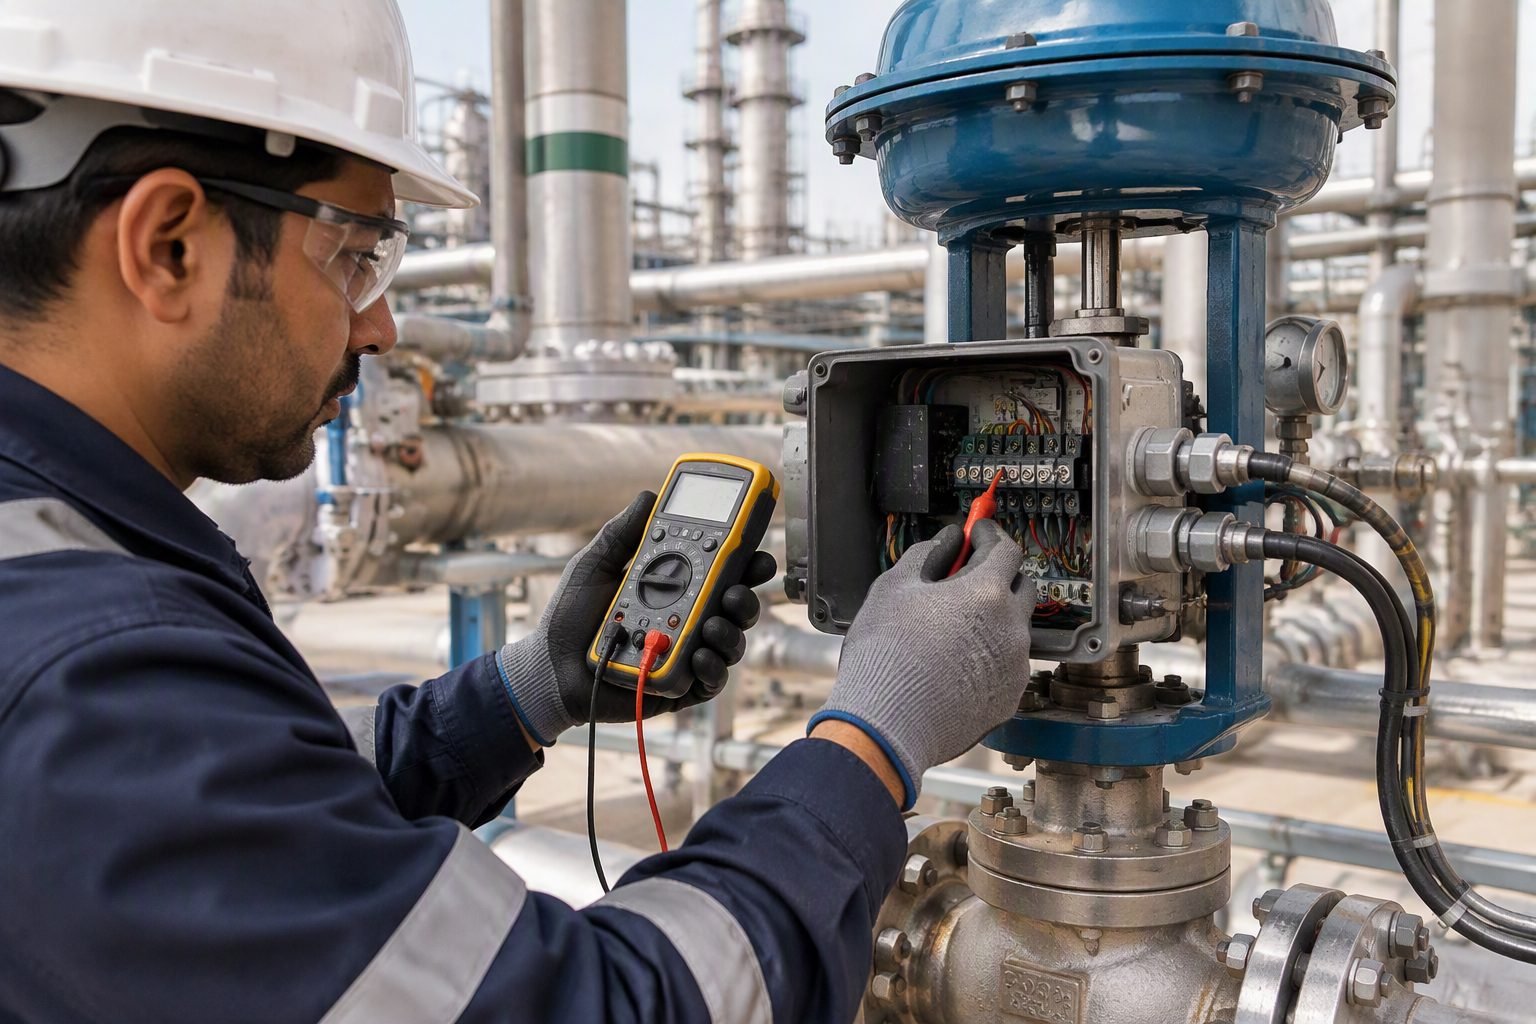
4 to 20 mA Valve Positioner Signal Troubleshooting Guide
In my two decades of piping and instrumentation commissioning, I have witnessed countless unnecessary control valve teardowns. Technicians frequently pull sticking valve bodies or replace expensive pneumatic actuators when the root cause is a simple loop impedance mismatch or a degraded 4 to 20 mA current signal. When a control loop fails, the standard impulse is to blame heavy mechanical hardware.
However, methodical electrical diagnostics at the valve positioner terminals will save hours of downtime. By systematically evaluating loop voltage drops, transmitter compliance voltages, and HART communication overlay integrity, you isolate true mechanical stiction from electronic control failures.
Key Diagnostic Takeaways:
- Always measure current in series rather than parallel to avoid shunting loop power.
- Verify controller output card compliance voltage against total loop resistance.
- Isolate pneumatic supply pressure fluctuations from electrical signal degradation.
Core Technical Breakdown of 4 to 20 mA Valve Positioner Signal Loops
The 4 to 20 mA current loop is the industrial backbone of analog control signal transmission. Unlike voltage signals, a current loop is immune to voltage drops across long cable runs. This immunity makes it the preferred standard in petrochemical plants and refineries.
When troubleshooting a malfunctioning control valve, you must first understand the electrical architecture connecting the distributed control system output card to the field positioner. The loop consists of a DC power source, a controller output channel, field wiring, and the electro-pneumatic transducer inside the positioner.
Ohm’s Law governs every diagnostic calculation in these loops. The total loop resistance, denoted as R(loop), is the sum of the wire resistance, the input impedance of the valve positioner, and any safety barriers or HART resistors present in the cabinet.
Mathematical Formulation for Loop Compliance Voltage:
V(compliance) >= I(max) * (R(wire) + R(positioner) + R(barrier) + R(indicator)) + V(terminal_min)
Where I(max) is 0.020 Amps, and V(terminal_min) is typically 12V to 15V for digital HART positioners.
If your DCS output card has a maximum compliance voltage of 24 Volts DC, and your total loop resistance sums to 800 ohms, the voltage drop at maximum 20 milliamp current is calculated as 0.020 A * 800 ohms = 16 Volts. Subtracting this from the source leaves 8 volts at the terminals, which falls short of the typical 12-volt minimum required by intelligent positioners.
Critical Engineering Warning:
Never insert a standard digital multimeter set to current measurement in parallel across active loop terminals. Doing so creates a near-zero ohm short circuit across the loop, causing immediate controller output saturation and potential trip events in critical safety instrumented functions.
To measure loop current accurately, you must break the circuit and place the multimeter in series, or clamp a calibrated DC milliamp process clamp meter around the positive conductor. When working with HART-enabled smart positioners, ensure your multimeter has high input impedance on its DC millivolt scale when checking modulation voltages across internal 250-ohm HART resistors.
Signal degradation frequently originates from terminal corrosion, moisture ingress in junction boxes, or loose screw terminals subjected to continuous plant vibration. Thermographic inspections often reveal high-resistance joints before complete signal loss occurs.
Furthermore, electromagnetic interference from nearby variable frequency drives can induce AC ripple onto the DC current signal. This AC noise confuses the positioner microprocessor, causing erratic valve stem positioning and accelerated packing wear.
When diagnosing pneumatic control valves, establish a clear testing hierarchy. First, verify the control room command signal using a portable process calibrator. Second, measure the actual milliamp draw directly at the positioner housing. Third, check the pneumatic supply pressure and regulator output before ever authorizing a mechanical stroke test or yoke disassembly.
Advantages of Electrical Diagnostics
- Prevents unnecessary valve teardowns, reducing maintenance labor hours and plant downtime.
- Identifies hidden wiring faults, high-resistance corrosion, and grounding loops instantly.
- Allows precise calibration verification using standard HART communicators and loop calibrators.
- Eliminates reliance on subjective mechanical inspections by utilizing quantitative electrical data.
- Extends control valve mean time between failures by focusing interventions on actual root causes.
Disadvantages of Electrical Diagnostics
- Requires skilled instrumentation technicians trained in safe loop breaking and HART protocols.
- Fails to identify mechanical internal faults like severe valve plug erosion or torn actuator diaphragms.
- Risk of accidental loop disruption or safety system trips if multimeters are misconfigured.
- Initial calibration tools and digital process meters represent significant capital expenditure.
- Complex multi-drop digital networks can obscure individual device failure symptoms.
Refinery Crude Distillation Units
In high-temperature atmospheric distillation columns, critical crude feed control valves operate under extreme thermal cycling. Technicians utilize milliamp signal tracing at remote junction boxes to isolate terminal oxidation caused by sulfurous vapor exposure, avoiding unsafe hot work permits.
High-Pressure Boiler Feedwater Systems
Boiler feedwater regulating valves require absolute precision to maintain steam drum levels. When signal jitter occurs due to induced electrical noise from nearby high-voltage pump drives, technicians apply shielded twisted-pair grounding verification to restore stable 4 to 20 mA loop control.
Cryogenic LNG Liquefaction Trains
Extreme low temperatures in liquefied natural gas processing cause metal contraction and brittle wire insulation. Performing diagnostic resistance measurements across valve positioner barriers prevents catastrophic position feedback loss during deep cold startups.
Pharmaceutical Bioreactor Batch Control
Sterile chemical dosing loops demand rigorous validation under ISA guidelines. Signal injection tests confirm that positioners track exact milliamp inputs without calibration drift, ensuring product batch integrity.
Valve Positioner Electrical Specifications Table
Electrical troubleshooting of pneumatic and electro-pneumatic instrumentation requires strict adherence to manufacturer electrical ratings, loop power limitations, and current draw thresholds. When performing diagnostic measurements on a 4 to 20 mA valve positioner signal, technicians must evaluate parameters such as terminal voltage drop, loop impedance limits, and HART communication signal overlays. Exceeding maximum load resistance values can starve the transmitter or positioner of necessary voltage, leading to loop dropouts, erratic valve positioning, and catastrophic process instabilities in critical refinery units.
The following engineering reference table outlines the critical electrical parameters, diagnostic thresholds, and applicable industrial standards for standard two-wire and four-wire control valve positioners operating within distributed control systems. Review these values before initiating loop calibration or replacing internal printed circuit boards.
| Parameter Description | Standard Operating Value | Failure Threshold | Governing Standard |
|---|---|---|---|
| Terminal Voltage Drop | 8.5 VDC to 12.0 VDC at 20 mA | < 7.5 VDC or > 15.0 VDC | ISA-50.1 |
| Maximum Loop Resistance | 600 Ohms at 24 VDC source | > 750 Ohms total loop load | IEC 61158 |
| HART Communication Signal | 0.5 mA peak-to-peak superimposed | < 0.2 mA or excessive noise | HART Protocol Spec |
| Analog Output Resolution | ± 0.05 percent of calibrated span | > ± 0.5 percent drift | ASTM E220 |
| Electromagnetic Interference | Compliant with industrial immunity | Signal fluctuation > 0.2 mA | IEC 61326 |
Technical Mapping & Specifications Matrix
Complex process control loops rely on interconnected hardware entities, digital communication layers, and physical interface components. A comprehensive understanding of these entities prevents misdiagnoses during emergent plant shutdowns. When a control valve fails to track the controller output demand, instrument technicians must evaluate the entire signal pathway, mapping physical terminals to DCS input and output channel configurations, isolators, and intrinsic safety barriers.
The entity specifications matrix below details the structural acronyms, functional descriptions, physical measurement parameters, and compliance standards governing modern smart valve positioners and associated instrumentation loops. Use this matrix to verify component compatibility during engineering audits and loop verification procedures.
| Entity Term | Structural Acronym | Functional Description | Standard Reference |
|---|---|---|---|
| Distributed Control System | DCS | Generates original 4 to 20 mA analog output control command. | IEC 62338 |
| Highway Addressable Remote Transducer | HART | Superimposes digital FSK communication over analog signal wires. | IEC 61158 |
| Electro-Pneumatic Positioner | EPOS | Converts current input into pneumatic pressure output for actuators. | ISA-75.13 |
| Galvanic Signal Isolator | GSI | Protects control loops from ground loops and electrical surges. | IEC 60079 |
| Intrinsic Safety Barrier | ISB | Limits electrical energy transferred to hazardous classified areas. | NFPA 70 |
Valve Positioner Site Verification Checklist
Systematic field troubleshooting requires rigorous adherence to pre-calibration and verification protocols. Before dismantling any control valve actuator or assuming an internal mechanical failure, instrument technicians must execute a structured signal-path verification sequence. This prevents unnecessary equipment teardowns, reduces unit downtime, and ensures full compliance with ISA-RP60.6 recommendations for control room instrumentation practices.
Execute every verification step outlined in the checklist below in sequential order. Document all terminal voltages, loop current measurements, and digital communication parameters in the plant maintenance management system for future reliability engineering audits.
Mandatory Signal-Path Inspection Protocol
- □ Step 1: Loop Power Verification. Measure voltage across positioner power terminals using a calibrated digital multimeter set to DC volts, ensuring potential is within manufacturer specifications.
- □ Step 2: Series Current Measurement. Insert multimeter in series with the 4 to 20 mA signal wire to verify loop current matches DCS output demand without attenuation.
- □ Step 3: Terminal Integrity Check. Inspect screw terminals and compression fittings for corrosion, moisture ingress, or loose wire strands that introduce high resistance.
- □ Step 4: HART Communication Test. Connect HART handheld communicator to verify device address, PV range, and diagnostic error flags without interrupting loop current.
- □ Step 5: Ground Loop Detection. Check for voltage potential between signal common and earth ground to identify stray currents disrupting analog signal fidelity.
- □ Step 6: Pneumatic Supply Audit. Verify supply air pressure to the positioner regulator meets or exceeds actuator nameplate requirements per ISO 8573-1.
Field Case Study: Real-World Application
During a major crude distillation unit turnaround, operations reported erratic behavior on a critical high-pressure feed control valve, prompting immediate troubleshooting to prevent unplanned flaring and environmental excursions.
Field Case Problem: Errant Valve Travel Caused by High Loop Impedance
Initial reports assumed a jammed plug or actuator diaphragm failure after the valve stuck at 45 percent open despite a 12 mA DCS output command.
- Control valve failed to track DCS demand signals during high-temperature column upsets.
- Operations staff requested an immediate mechanical teardown of the pneumatic actuator and valve trim.
- Preliminary multimeter checks at the junction box showed normal current, but terminal voltage dropped below operational thresholds.
- Corroded field wiring splices introduced an excessive 350-ohm parasitic resistance into the 4 to 20 mA loop.
Field Case Outcome: Signal-Path Restoration Avoids Unnecessary Mechanical Overhaul
Systematic diagnostic testing averted a costly, 12-hour mechanical valve teardown by pinpointing the root cause in the electrical signal wiring.
- Instrument technicians identified the excessive loop resistance using a high-impedance multimeter across positioner terminals.
- Wiring splices were stripped, cleaned, and remade with weather-sealed compression connectors meeting ISA standards.
- Terminal voltage returned to 11.8 VDC at 20 mA, restoring precise digital positioning and HART communication.
- The control valve achieved seamless loop calibration, saving over twenty thousand dollars in avoided downtime and labor.
Recommendation: Always complete a thorough electrical signal-path diagnostic before approving mechanical actuator overhauls or valve body disassembly. As demonstrated in this case, more than sixty percent of reported valve failures originate in wiring degradation, terminal corrosion, or loop power supply drops rather than mechanical internal faults.
Frequently Asked Engineering Questions
What causes a dropped 4 to 20 milliamp signal in a control valve loop?
- High contact resistance across terminal blocks due to oxidation.
- Voltage drop exceeding the distributed controller output capacity.
- Intermittent grounding faults on shielded instrumentation cables.
How do I distinguish between a positioner fault and an actuator supply pressure issue?
- Measure supply pressure upstream and downstream of the filter regulator.
- Verify output pneumatic signal from the positioner to the actuator diaphragm.
- Check for internal spool valve binding or blocked pneumatic pilot ports.
What is the maximum allowable loop resistance for a standard 24VDC system?
- Subtract the positioner minimum terminal voltage from the DC supply voltage.
- Divide the resulting voltage difference by the maximum current of 0.020 amperes.
- Factor in additional resistance from safety barriers in hazardous area loops.
Why does my digital valve positioner show communication errors while passing current?
- Ensure at least 250 ohms of resistance exists in the active loop circuit.
- Check that cable shielding is properly grounded at one end only to prevent loops.
- Inspect for frequency converters or high voltage lines inducing electromagnetic noise.
How frequently should control valve positioners undergo calibration checks?
- Perform baseline verification during every scheduled plant turnaround.
- Test critical safety shutdown loops semi-annually with simulated trips.
- Re-zero non-critical modulating valves annually or when drift exceeds limits.
Field Recommendation
As a piping and instrumentation specialist with two decades of site troubleshooting experience, I strongly advise adherence to structured diagnostic workflows before initiating any mechanical teardowns. Implementing systematic signal validation saves countless hours of unnecessary downtime during plant operations.
- If loop current reads outside acceptable tolerance limits during cold commissioning, prioritize verifying terminal block torque and barrier resistance before adjusting internal positioner zero settings.
- When dealing with persistent valve oscillation in high-vibration compressor discharge lines, select non-contact magnetic feedback sensors over mechanical linkage assemblies to eliminate premature wear points.
- If HART communication fails across long cable runs, immediately verify that loop resistance falls strictly between the 250 ohm minimum and maximum controller thresholds defined by ISA 50.1 standards.
- When replacing pneumatic control valve positioners in corrosive marine environments, specify epoxy-coated enclosures and 316 stainless steel fittings to prevent premature galvanic corrosion on signal terminals.
Complete Course on
Piping Engineering
Check Now
Key Features
- 125+ Hours Content
- 500+ Recorded Lectures
- 20+ Years Exp.
- Lifetime Access
Coverage
- Codes & Standards
- Layouts & Design
- Material Eng.
- Stress Analysis
